
Aluminum welding and repair
We weld and repair aluminum at our Reno shop as part of our welding, all types: cracked housings, tanks and other aluminum parts, plus welded aluminum assemblies. The process takes more care than steel because of the oxide skin, the way aluminum pulls heat away and how easily thin walls distort.
- Built from your specifications, drawings or samples
- Free consultations, prompt estimates
- Wolf Machine stands behind the work we perform
- Reno shop, Monday to Friday, 7:00 am to 3:30 pm
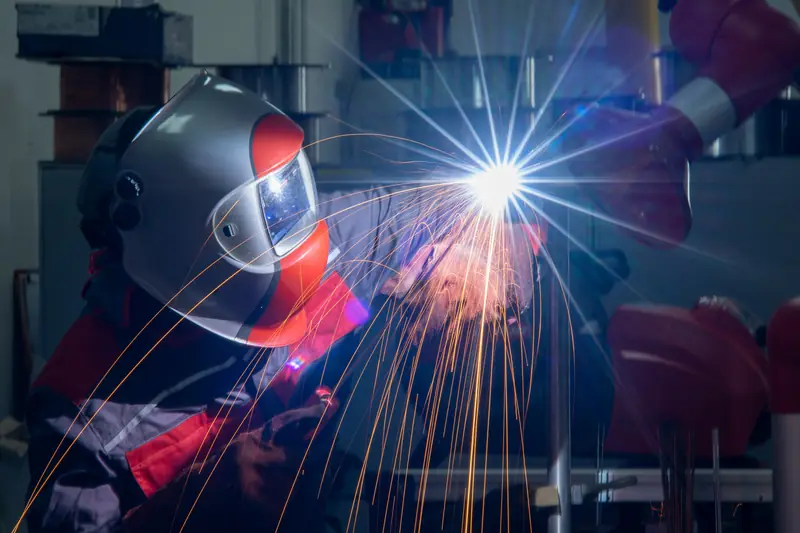
Stock photo: TIG (gas tungsten arc) welding, close up
Aluminum welds well when it is clean and the heat is controlled, and it spoils quickly when it is not. This page is about the joint and the process. If you want to know how aluminum cuts and what grades are used, the aluminum material page covers that.
At a glance
- Oxide removed from the joint before welding
- Filler matched to the alloy family
- Heat managed to limit distortion and burn-through
- Repairs to cast and wrought aluminum parts
- Welding, all types, with machining in the same shop
Love working with these guys, and gal. Great customer service and knowledgeable skill base. They have helped with many big projects and have always pulled though when our machines went down.
The oxide skin and why cleaning comes first
Bare aluminum is covered by a thin oxide layer that melts at a much higher temperature than the metal underneath. If it is left in the joint, the weld pool cannot flow together cleanly and the weld ends up porous or weak.
So the joint is cleaned right before welding: degreased, then the oxide is brushed or cut away with tools used only on aluminum. Oil, paint and moisture trapped in a crack cause the same trouble, which is why a dirty repair on an old housing takes extra prep.
Heat goes somewhere else in aluminum
Aluminum carries heat away from the weld quickly, so it takes more heat to start a weld, and then the part holds that heat and can sag or burn through. Thin walls are the hardest case. The usual answers are tight fit-up, backing and clamps, and short, controlled welds that let the part cool.
Distortion is the other side of the same coin. On a machined housing, a weld that pulls the part out of flat can ruin a fit, so the plan often leaves extra material to machine after welding.
Filler depends on the alloy family
Aluminum is sold in families, and the filler wire has to suit the base metal. Common 6xxx wrought alloys and 5xxx alloys weld with different fillers, and some high-strength alloys are poor candidates for fusion welding at all. Cast aluminum often has porosity and trapped oil that make repairs more delicate.
If you know the alloy, say so. If you do not, a photo of the part, its use and any stamped markings give us a starting point, and we can look at the part before promising a repair.
Why cast aluminum parts crack and what to send
Cast aluminum parts usually crack at sharp corners, thin sections, mounting bosses and places that see vibration or impact. A repair that does not address the stress will crack again beside the weld.
For a quote, send the following and we will review it during shop hours at 4812 Longley Ln, Reno.
- Photos of the crack from two sides, with a ruler in the shot
- Whether the part is cast or machined from bar, if you know
- What the part does and what loads or heat it sees
- The machine or equipment it came from
Sources
- The Aluminum Association (2026-10-18)
- OSHA 29 CFR 1910.252, Welding, cutting and brazing: general requirements (2026-10-18)
Aluminum repairs people bring
- Cracked cast housings and covers
- Broken brackets and mounting ears
- Tanks and enclosures with split seams
- Frames that need a weld repair
- Welded aluminum assemblies built to a drawing
Typical parts
- Cast housings
- Brackets
- Tanks
- Frames
- Cast housings
How to send us the job
Send a drawing (PDF, DWG, DXF, STEP or IGES), a sketch with sizes, or photos of the part with a tape or scale in the shot. A sample works too: bring it to the shop.
Questions about this service
From the shop
Work from the shop
Straight answers
Aluminum welding questions
Still have a question? Call (775) 359-5570, Monday to Friday, 7:00 am to 3:30 pm.
Can aluminum always be welded?
Most common aluminum alloys can be welded, but some high-strength alloys and heavily oil-soaked castings are difficult. We look at the part first and tell you what is realistic.
Do you weld aluminum and then machine it?
Yes. A welded boss or housing can be milled or bored back to size after welding, which is why we leave extra material when the plan calls for it.
Send us the job
Request a quote
Tell us what you need, attach a drawing or photos of the part, and we will get back to you during shop hours. Free consultations; prompt estimates.
- From your specifications, drawings or samples. We can also assist you in designing your product or part.
- Free consultations and prompt estimates
- Stands behind the work: Our rates are very competitive and our quality is second-to-none. Wolf Machine stands behind the work we perform.
- Company accounts: all major credit cards, or we can open an account for your company
Shop hours Monday to Friday, 7:00 am to 3:30 pm. Send your request any time and we will get back to you during shop hours.
Stock photo: a lathe turning a bar, hot chips flying