
Stainless steel welding that keeps the metal stainless
We weld stainless steel at our Reno shop, including strainers, baskets, tubes and plant parts. The goal of a stainless weld is not only strength, it is to keep the corrosion resistance that made you choose stainless in the first place.
- Built from your specifications, drawings or samples
- Free consultations, prompt estimates
- Wolf Machine stands behind the work we perform
- Reno shop, Monday to Friday, 7:00 am to 3:30 pm
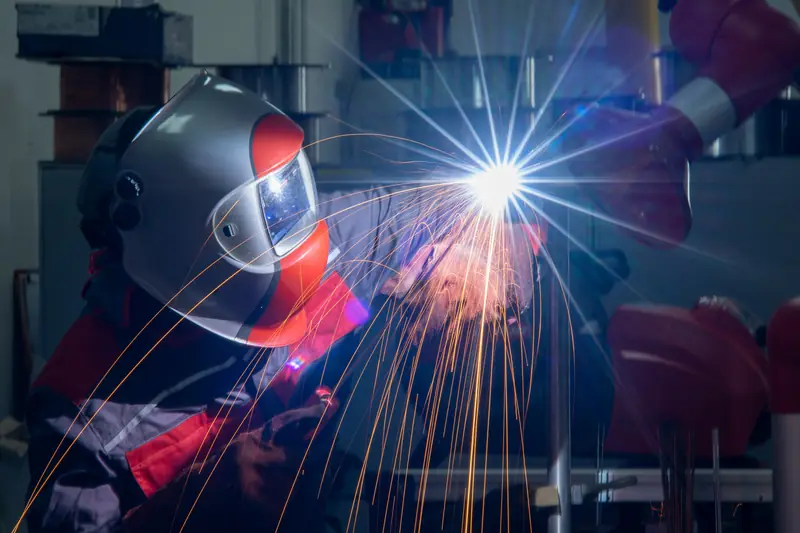
Stock photo: TIG (gas tungsten arc) welding, close up
Stainless resists rust because of a thin chromium-rich film on the surface. Welding can damage that film, so the joint is where stainless parts most often fail in service. This page covers the weld, the heat and the cleanup. How stainless machines is a separate subject on the material page.
At a glance
- Heat kept down to protect corrosion resistance
- Clean joints, with tools used only on stainless
- Strainers and baskets seam-welded to flanges
- Stainless parts for food processing plants
- Ventilation and fume control as a standard part of the work
I have used Wolf Machine several times over the past few years for fabricating and repair of parts on my ultralight aircraft. [...] These guys are great to deal with. I wouldn't take my projects anywhere else.
Why heat is the enemy of stainless corrosion resistance
Stainless gets its name from chromium. When the metal sits too long in a certain heat range during welding, chromium can combine with carbon near the weld, and the area beside the weld loses some of its protection. This is called sensitization, and it is the reason a stainless weld can rust or corrode in service even though the base plate does not.
The practical answer is controlled heat: stringer passes instead of wide weaves, time to cool between passes, and filler suited to the grade. Low-carbon grades are also chosen for welded parts for this reason. A heat-affected zone is always there. The job is keeping it narrow.
Cleanliness and finishing the joint
Carbon steel dust, grinding dust or a steel wire brush can embed iron in a stainless surface and cause rust spots later. Stainless is cleaned and ground with tools kept for stainless only.
After welding, the heat tint around a weld is a sign of a disturbed surface. In many food and washdown applications the joint is cleaned back and passivated, a general practice that restores the protective film. Tell us at quote time if a part has a finish requirement, so the plan includes it.
Distortion and thin sheet
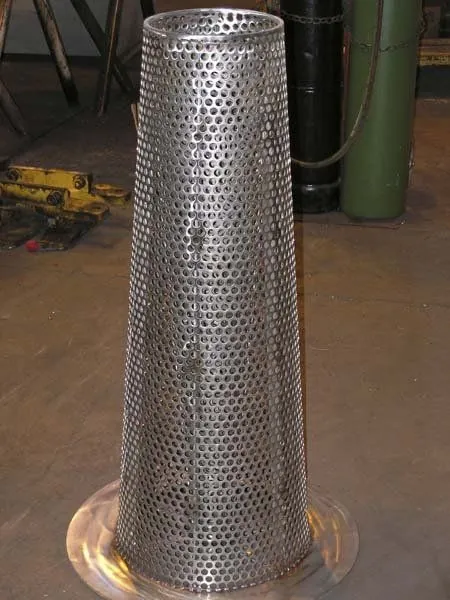
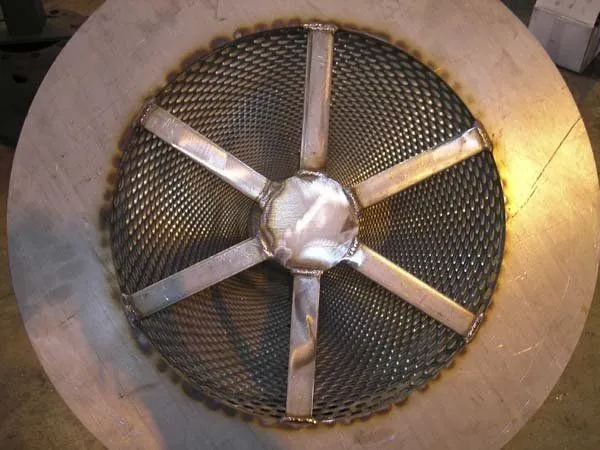
Stainless expands more than carbon steel and conducts heat poorly, so it warps easily, especially in thin sheet. Perforated strainer sheet seam-welded into a cone and then to a flange is a good example: the welds have to be placed and sequenced so the shape stays round and the flange stays flat.
Food-plant parts and fume control
Our services list includes steam tubes, titanium screws, handles and stainless steel knives made for a food processing plant. That kind of work shows why joints must be smooth and clean.
Welding stainless creates fume that can contain hexavalent chromium, which is why shops ventilate and follow the exposure rules in OSHA 29 CFR 1910.1026. You can read more in our post on the OSHA rules behind stainless welding.
- Send the grade if it is stamped or on the drawing
- Say whether the part sees food, water, chemicals or heat
- Include photos of the break or a drawing of the new part
Sources
- Stainless steel (overview) (2026-10-18)
- OSHA 29 CFR 1910.1026, Chromium (VI) (2026-10-18)
Stainless welding jobs
- Perforated strainers and baskets welded to flanges
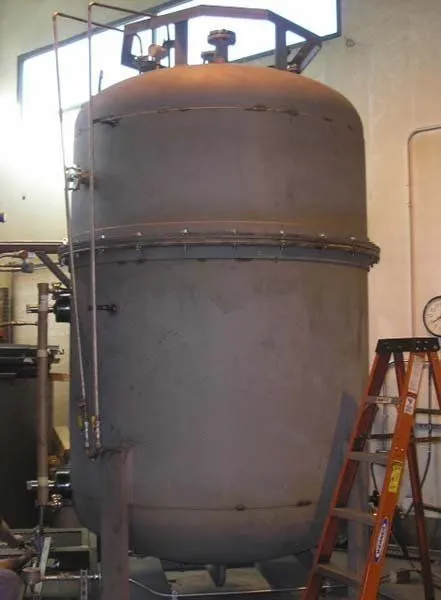
- Tanks and chutes for plant use
- Tube, handle and fitting repairs
- Plant parts for washdown areas
- Welded stainless assemblies built from a drawing
Typical parts
- Strainers and baskets
- Steam tubes
- Handles
- Chutes
- Brackets
How to send us the job
Have a print? Attach it to the quote request. No print? Photos of every face, the sizes you know and the machine the part came from are a good start, and you can bring the part in.
Related
Questions about this service
From the shop
Work from the shop
Metal and plastic fabrication
Related services
Straight answers
Stainless steel welding questions
Still have a question? Call (775) 359-5570, Monday to Friday, 7:00 am to 3:30 pm.
Why does stainless sometimes rust beside a weld?
Heat from welding can pull chromium out of the metal near the weld, which lowers its resistance to corrosion. Controlled heat, suitable filler and cleaning after welding reduce the risk.
Can you weld stainless to carbon steel?
Yes, with filler chosen for the combination. Tell us which two metals are being joined and what the part does, and we will say how we would build the joint.
Do you build stainless strainers and baskets?
Yes. Perforated stainless strainers seam-welded to flanges are part of our gallery. See the strainers and tanks page for more.
Send us the job
Request a quote
Tell us what you need, attach a drawing or photos of the part, and we will get back to you during shop hours. Free consultations; prompt estimates.
- From your specifications, drawings or samples. We can also assist you in designing your product or part.
- Free consultations and prompt estimates
- Stands behind the work: Our rates are very competitive and our quality is second-to-none. Wolf Machine stands behind the work we perform.
- Company accounts: all major credit cards, or we can open an account for your company
Shop hours Monday to Friday, 7:00 am to 3:30 pm. Send your request any time and we will get back to you during shop hours.
Stock photo: a lathe turning a bar, hot chips flying