4812 Longley Ln, Reno, NV 89502Mon-Fri 7:00 am - 3:30 pmMon-Fri 7:00 am - 3:30 pm(775) 359-5570
Wolf Machine & Fabrication, Inc.

Surface finish (Ra)

Ra is the arithmetic average roughness of a surface: the average height of the tiny peaks and valleys left by the cutting process, measured along a short line. It is written in microinches (millionths of an inch) in the US and micrometers elsewhere, and a smaller number means a smoother surface.

Have a drawing, a sample or a broken part? Call (775) 359-5570 or request a quote and attach your drawing or photos.

  • Built from your specifications, drawings or samples
  • Free consultations, prompt estimates
  • Wolf Machine stands behind the work we perform
  • Reno shop, Monday to Friday, 7:00 am to 3:30 pm

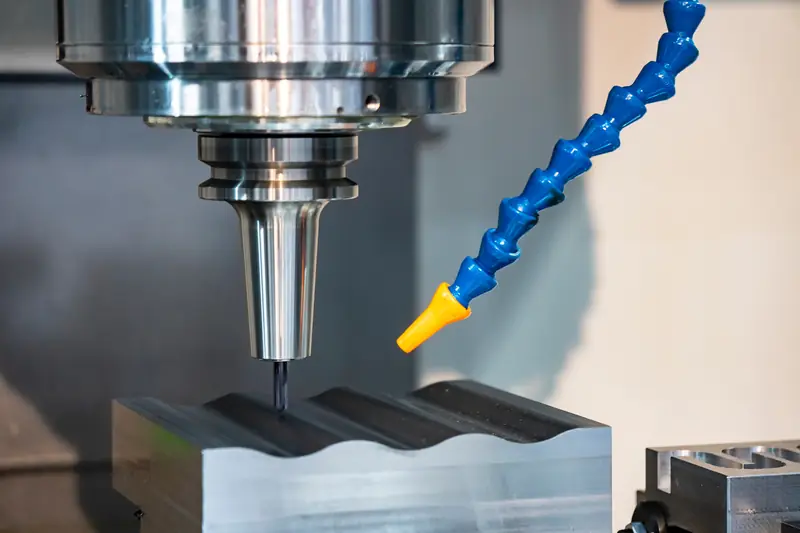
Stock photo: a milling cutter taking a finishing pass on a steel block, coolant line beside it

Look at a turned shaft under a lamp and you can see fine lines. Those lines are the tool marks, and their depth is what a finish callout puts a number on. A print might say 63 Ra on a bearing journal and leave a rough note on everything else, because only some surfaces need to be smooth.

Microinches and micrometers

One micrometer is about 40 microinches, so 32 microinches Ra is roughly 0.8 micrometers. Prints from US customers usually show microinches with a small check-mark symbol, while prints from metric drawings show micrometers. Either way, the number on the print is a ceiling: the surface may be that smooth or smoother.

Ra is an average, so it does not show a single deep scratch. For that reason a seal surface may carry an extra note, such as no spiral lead or no cross-scratches. The older RMS figure averages the same profile a different way and is covered with the other short entries on the glossary page.

Textbook ranges by process

These are general ranges for the processes, taken from standard machining references. They describe what the processes tend to produce in principle. They are education, not a statement of what any one shop holds, and the callout on your print is what sets the finish.

A rough turned or milled surface commonly falls in the low hundreds of microinches. A sharp tool and light feed commonly give tens of microinches. Grinding goes smoother still, and lapping or polishing smoother again. Each step down takes more time and care.

Where finish matters on a part

Finish matters most where one part touches or seals against another: bearing journals, seal diameters, sliding faces and sealing faces. A seal that runs on a surface that is too rough wears quickly, and a surface that is too smooth can fail to hold oil.

When a worn seal area has been rebuilt by metal spray or a sleeve, the surface is machined or ground back to the finish on the print. Put the finish callout on the drawing, or tell us the shaft or bore it goes with, when you send the quote request. A finish tighter than the part needs adds cost without adding function, as the tolerance entry also explains.

Sources

Talk to the shop

(775) 359-5570

Monday to Friday7:00 am - 3:30 pm
Saturday and SundayClosed
Request a quote

Send us the job

Request a quote

Tell us what you need, attach a drawing or photos of the part, and we will get back to you during shop hours. Free consultations; prompt estimates.

Call (775) 359-5570

  • From your specifications, drawings or samples. We can also assist you in designing your product or part.
  • Free consultations and prompt estimates
  • Stands behind the work: Our rates are very competitive and our quality is second-to-none. Wolf Machine stands behind the work we perform.
  • Company accounts: all major credit cards, or we can open an account for your company

Shop hours Monday to Friday, 7:00 am to 3:30 pm. Send your request any time and we will get back to you during shop hours.

Your quote request

Three short steps. Attach a drawing or photos if you have them; only your name and a phone or email are required.

Step 1 of 3: What you need
This request is for
Step 2 of 3: Drawings or photos

Attach drawings or photos (optional)

Up to 5 files, 12 MB in total. A photo of the part with a tape measure in the shot is enough to start. Used only to quote your job. Photos are resized before sending; drawings are sent as they are. Larger files: email them to [email protected].

Step 3 of 3: How we reach you

We review requests during shop hours, Monday to Friday, 7:00 am to 3:30 pm, and get back to you with questions or a prompt estimate. Free consultations.

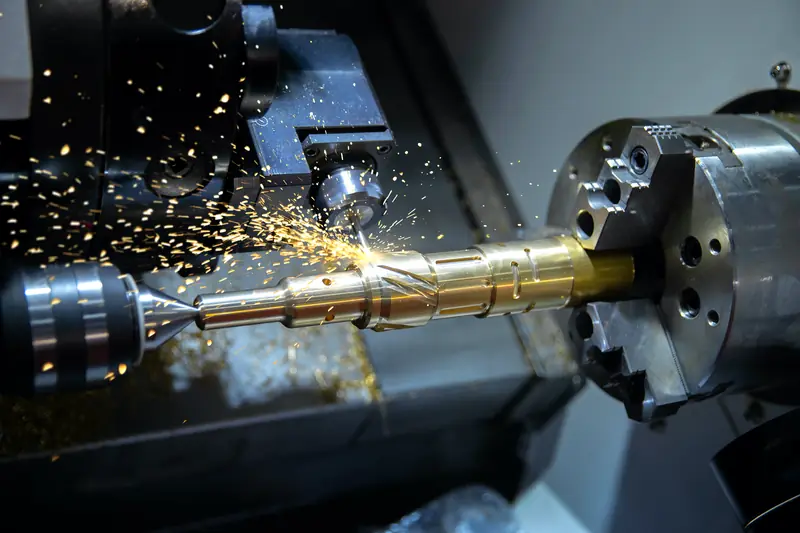
Stock photo: a lathe turning a bar, hot chips flying